Global packaging demand is becoming more automated, flexible, and data-driven. Smithers’ The Future of Global Packaging to 2028 estimates that the worldwide packaging market will approach approximately US$1.2 trillion by 2028. This growth increases pressure on manufacturers to select Carton Forming equipment that supports reliable output, shorter changeovers, and lower material waste. Carton Forming machines now serve food, beverage, pharmaceutical, personal care, and e-commerce operations with very different production conditions.
This guide examines the best carton forming machine types for global buyers in 2026. Horizontal cartoners suit products requiring controlled, precise loading. Vertical cartoners often support compact layouts and efficient dosing applications. Wraparound case formers provide strong transport protection, while robotic forming systems offer flexible handling for varied carton sizes. PMMI’s 2024 industry research continues to identify labor availability, automation, and operational efficiency as major packaging investment drivers. These factors make servo-driven forming, tool-free adjustment, remote diagnostics, and quick format changeovers increasingly valuable.
However, the fastest machine is not always the best purchase. A high-speed former may struggle with recycled board, unstable blanks, dusty products, or frequent size changes. That assumption needs review. Buyers should compare forming speed, board compatibility, glue performance, footprint, safety systems, service response, and total cost of ownership. EUROMAP and global packaging machinery guidance also emphasize responsible machine integration, operator safety, and lifecycle performance. Real factory experience matters here: a machine should form clean corners at the end of a long shift, not only during a demonstration. The following overview connects machine design with practical production risks, helping international buyers make a more evidence-based decision.
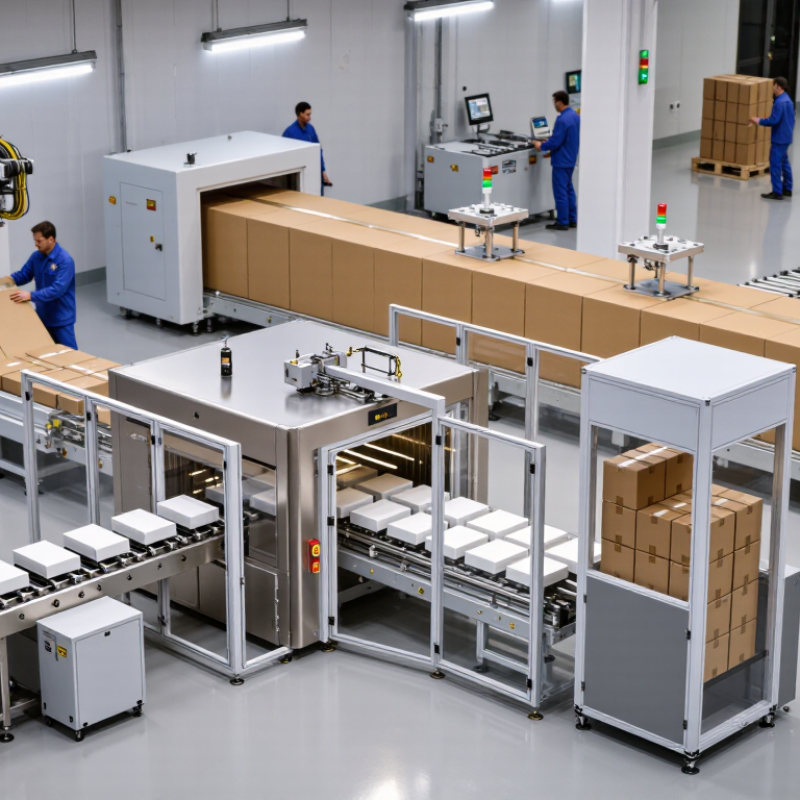
A carton forming machine converts flat carton blanks into usable three-dimensional packages. It feeds, folds, squares, and closes each carton with controlled mechanical movement. Depending on the design, closure may use adhesive, tuck flaps, or locking tabs.
The process usually begins with a magazine that stores die-cut blanks. A vacuum or friction feeder separates each blank and moves it toward forming tools. Folding rails create accurate creases, while guides keep the carton square. Some machines add glue through a metering system. Sensors check blank position, flap movement, and carton discharge.
Carton forming machines serve food, household, pharmaceutical, and industrial packaging lines. Their performance depends on board thickness, coating, crease quality, and carton dimensions. In field testing, a machine may run smoothly with one carton size but struggle after a minor design change.
This matters.
A reliable evaluation should include speed, changeover time, compressed-air use, access for cleaning, and operator safety. Ask for test results using your actual blanks. A polished demonstration can hide feeding problems. Sometimes, slower forming produces better carton geometry and fewer jams. The fastest setting is not always the best setting. Each buyer should verify tolerance, maintenance support, and local electrical requirements before installation.
Carton forming machines turn flat carton blanks into accurate three-dimensional packages. Their operation looks simple, but each movement needs precise timing. A magazine holds the blanks in a controlled stack. Vacuum cups pick one blank and transfer it toward the forming section. Guide rails position the board before folding begins. The machine applies adhesive or prepares locking tabs, depending on the carton design. Folding arms and forming tools then raise panels around a fixed shape. Pressure belts keep the carton square while the adhesive sets.
Sensors monitor blank position, flap movement, and possible jams. When timing is correct, formed cartons move smoothly to the discharge conveyor. Small adjustments matter. For global buyers, the machine type should match carton style, board thickness, and required output. Intermittent machines suit varied carton sizes and frequent changeovers. Continuous systems can provide higher speed when production remains stable. Some lines also include automatic blank feeding, glue inspection, and carton counting.
Real production is less tidy. Dust, warped blanks, and humidity can affect suction and folding. A common lesson is that a powerful motor cannot fix poor carton alignment. This detail is easy to miss. Buyers should request test runs using their actual board and carton dimensions. They should measure squareness, glue position, changeover time, and reject rates. A specification sheet helps, but sample cartons reveal more. Even a well-designed machine may need better guides after installation.
Main Types of Carton Forming Machines in 2026
Carton forming machines are becoming more specialized as packaging lines handle smaller batches and varied carton sizes. Smithers’ The Future of Folding Cartons to 2028 reports continued global growth in folding carton demand, supported by food, beverage, healthcare, and household packaging. This trend increases interest in flexible forming equipment.
The main types include tuck-in carton formers, glue-sealing machines, lock-bottom formers, wrap-around case packers, and tray erectors. Tuck-in machines suit lightweight cartons and fast retail packaging. Glue-sealing models provide stronger closures, especially for heavier products. Lock-bottom machines create a stable base without additional manual folding. Wrap-around systems form cartons directly around products, saving space during transport. Tray erectors are common where open-top presentation matters.
Each type has practical limits. A glue system needs accurate adhesive control and clean maintenance. A lock-bottom machine may require more precise board scoring. The choice is not always obvious. According to PMMI packaging machinery research, labor shortages and automation remain major investment drivers in packaging operations. Buyers should therefore examine changeover time, board quality, speed stability, and operator access.
A machine rated for 300 cartons per minute may perform differently with recycled board or small cartons. That detail is often missed. Independent trials using actual carton blanks can reveal feeding problems before installation. Buyers should also compare energy use, spare-part availability, safety guarding, and technical training. A cheaper machine can become expensive when adjustments are frequent.
| Machine Type | Primary Carton Style | Typical Forming Method | Typical Speed Range | Common Board Range | Recommended Applications | Automation Level | Main Purchasing Considerations |
|---|---|---|---|---|---|---|---|
| Vertical Carton Erector | Regular Slotted Carton Bottom-Taped Box | Flat corrugated blanks are opened vertically, squared, and sealed at the bottom with tape or hot-melt adhesive. | 8–25 cartons/min | Approx. 3–7 mm corrugated board | General case packing, food ingredients, household products, and warehouse distribution cartons. | Automatic or semi-automatic | Carton size range, blank magazine capacity, sealing method, compressed-air requirements, and floor space. |
| Horizontal Carton Erector | Flat-Folded Case RSC Carton | Carton blanks are fed and opened horizontally before bottom flaps are folded and sealed. | 10–30 cartons/min | Approx. 3–7 mm corrugated board | High-throughput packaging lines where cartons are transferred directly to filling or case-packing equipment. | Automatic | Infeed orientation, line integration, carton stability, format changeover, and conveyor height. |
| Wraparound Case Packer | Wraparound Carton Tray with Hood | A flat blank is wrapped around grouped products and sealed to create a tight transport case or display-ready pack. | 15–60 packs/min | Approx. 1.5–4 mm corrugated board | Bottles, cans, cartons, trays, multipacks, and retail-ready secondary packaging. | Automatic | Product collation accuracy, blank quality, hot-melt performance, compression control, and pack dimensions. |
| Tray Former | Open Tray Display Tray | Die-cut blanks are folded and locked or glued to form shallow trays with open tops. | 10–40 trays/min | Approx. 0.5–3 mm paperboard or corrugated board | Produce, bakery items, beverage multipacks, promotional displays, and shelf-ready packaging. | Automatic or semi-automatic | Tray height, corner-lock design, board stiffness, product loading method, and display requirements. |
| Four-Corner Box Former | Four-Corner Box Rigid Folding Carton | Pre-creased blanks are folded at four corners and bonded with adhesive to create a rigid, square container. | 10–35 boxes/min | Approx. 0.7–1.5 mm folding carton board | Food, cosmetics, small consumer goods, gift packs, and premium retail packaging. | Automatic | Corner accuracy, glue pattern, compression time, board grain direction, and finished-box squareness. |
| Six-Corner Box Former | Six-Corner Box Premium Folding Box | Multiple pre-creased panels are folded and glued to form a reinforced box with six bonded corners. | 8–30 boxes/min | Approx. 0.7–1.5 mm folding carton board | Premium food packaging, electronics accessories, personal-care products, and gift boxes. | Automatic | Complexity of the blank, glue control, folding sequence, setup precision, and product presentation quality. |
| Lock-Bottom Carton Former | Auto-Lock Bottom Crash-Lock Box | Pre-glued folding cartons are opened and the interlocking bottom panels are folded into a self-locking base. | 15–50 cartons/min | Approx. 0.3–0.8 mm folding carton board | Pharmaceuticals, cosmetics, food products, hardware, and retail cartons requiring quick bottom locking. | Automatic | Locking reliability, carton memory, blank crease quality, product insertion speed, and changeover time. |
| Straight-Line Gluer Former | Straight-Line Carton Tuck-End Box | Printed and die-cut blanks are folded along crease lines and bonded in a continuous straight-line process. | 30–150 m/min line speed | Approx. 0.25–0.8 mm folding carton board | High-volume retail cartons for food, pharmaceuticals, cosmetics, and everyday consumer products. | Automatic | Line speed, feeder stability, glue-system precision, fold quality, inspection, and downstream counting. |
| Partition and Divider Former | Cell Divider Bottle Partition | Interlocking paperboard or corrugated strips are folded and assembled into protective internal compartments. | 10–60 sets/min | Approx. 1–5 mm paperboard or corrugated board | Glass bottles, jars, laboratory containers, appliances, and fragile products requiring separation. | Automatic or semi-automatic | Cell dimensions, strip tolerances, assembly accuracy, material strength, and compatibility with the outer case. |
| Custom Die-Cut Carton Former | Specialty Carton Display Packaging | Custom-shaped blanks are folded, formed, and optionally glued according to a specific structural design. | 5–30 cartons/min | Approx. 0.3–4 mm, depending on substrate | Promotional packaging, unusual product geometries, retail displays, and short-run or multi-format production. | Semi-automatic or automatic | Blank complexity, tooling flexibility, format range, operator skill, trial production, and return on investment. |
Note: Speed, board thickness, and carton dimensions are typical industry ranges for 2026 planning purposes. Actual performance depends on carton design, substrate quality, adhesive system, product loading, machine configuration, and line integration.
Choosing a carton forming machine in 2026 requires more than comparing rated speed. The right model must fit your carton sizes, board materials, factory space, and daily workload.
Start with product dimensions and blank quality. Measure flat blanks, folded depth, and required sealing accuracy. A machine handling 1,200 cartons per hour may perform poorly with small boxes or thick corrugated board. Small gaps matter.
In production evaluations, changeover time deserves close attention. A practical test uses three carton sizes from your actual orders. Record adjustment steps and operator effort. Servo-driven systems can improve positioning, but they may require stronger technical skills.
For continuous runs, inspect glue control, compression timing, feeding stability, and reject rates. Ask operators to examine finished cartons. Their daily experience often reveals problems that brochures hide.
Energy use, floor space, and maintenance access also affect the decision. Confirm electrical requirements, guarding, noise limits, and applicable safety standards before installation. Reliable technical support should include clear manuals, training, and available wear parts.
Do not trust speed claims alone. A supplier may promise stable output, yet provide no test data for your carton design. That assumption can become expensive. I have seen buyers overlook dust control and cleaning access. The machine then loses accuracy after several weeks.
A slower model with easier adjustment may produce better results in real conditions. Perfect selection is unlikely. Careful testing reduces regret.
Carton forming machines support food, cosmetics, electronics, household goods, and industrial packaging worldwide. Common choices include intermittent-motion, continuous-motion, and robotic forming systems. Each type suits different carton sizes, board grades, and production targets. A machine running well in Germany may need changes for humid Southeast Asian conditions. Dust, temperature, and board moisture can affect feeding accuracy.
Global buyers should examine electrical compatibility, guarding, emergency stops, documentation, and operator training. Requirements often vary by country and factory. Ask for test runs using your actual carton blanks and adhesive. Check changeover time, reject rates, compressed-air use, and accessible maintenance points. Independent safety reviews can add confidence. However, certification alone does not guarantee reliable daily performance. Poor setup can still create jams and damaged cartons.
Tips: Request sample cartons before purchase. Confirm local service response times. Review spare-part availability and software language options. Leave room for future size changes. A perfect specification rarely exists. In practical evaluations, buyers sometimes overvalue maximum speed and overlook unstable feeding. That mistake can reduce usable output. Ask suppliers to record sustained performance, not only short demonstrations. A clear acceptance test should define speed, quality, noise, and downtime limits. Allow operators to inspect the machine directly. Their feedback may reveal awkward access or cleaning problems that technical sheets miss.

