10 Best Rubber Automatic Cutting Machines for Buyers
Choosing a Rubber Automatic Cutting machine is not simply a matter of comparing speed claims. Rubber varies widely in thickness, hardness, and flexibility, from thin gasket sheets to dense industrial matting. A cutter suited to one material may struggle with another. Small details matter.
This guide to the 10 best machines for buyers focuses on practical factors: cutting area, material capacity, blade type, control system, and setup requirements. It also considers how each machine may fit a real production floor. For example, a shop cutting flat EPDM sheets may need a different setup from a manufacturer processing silicone rolls or custom seals. Ask suppliers about sample cuts using your own material. A clean edge on a brochure is not proof of consistent results in daily production.
Automation can reduce repetitive handling, but it does not remove every production challenge. Operators still need suitable training, clear maintenance routines, and a safe way to load and unload material. Check how easily the machine handles changing jobs, and whether its software supports the file formats your team already uses. Noise, floor space, extraction needs, and service access deserve attention too. They are easy to overlook.
The rankings are a starting point, not a universal verdict. Some specifications are difficult to compare across brands, and advertised throughput may depend on material and job complexity. Consider your workload, budget, and local service options before deciding. The best choice is the one that performs reliably on your parts, not merely the one with the longest feature list.
Rubber Cutting Fundamentals: Shore A Hardness Testing under ASTM D2240
Shore A hardness testing helps buyers compare rubber materials before choosing an automatic cutting machine. Under ASTM D2240, a durometer measures resistance to indentation; it does not directly measure tensile strength or cutting ease. A steady, flat test surface matters. So does sample preparation. A cutting machine can produce coupons with consistent edges, but the test method governs specimen dimensions and conditioning. Follow the applicable standard and material instructions rather than assuming one sample size suits every rubber.
Keep samples at a controlled temperature and let them condition before testing. Check the durometer’s calibration, place its presser foot flat, and avoid edges or visibly damaged areas. Take readings at separated points and record the test conditions; rubber can vary across a sheet. Small details count. A clean cut is useful, but it does not prove uniform hardness. One limitation is easy to overlook: a neat coupon may still fail to represent a nonuniform batch. Shore A results are best treated as one purchasing check, alongside thickness, formulation data, and trial cutting on the intended material.
10 Best Rubber Automatic Cutting Machines for Buyers — Rubber Cutting Fundamentals: Shore A Hardness Testing under ASTM D2240
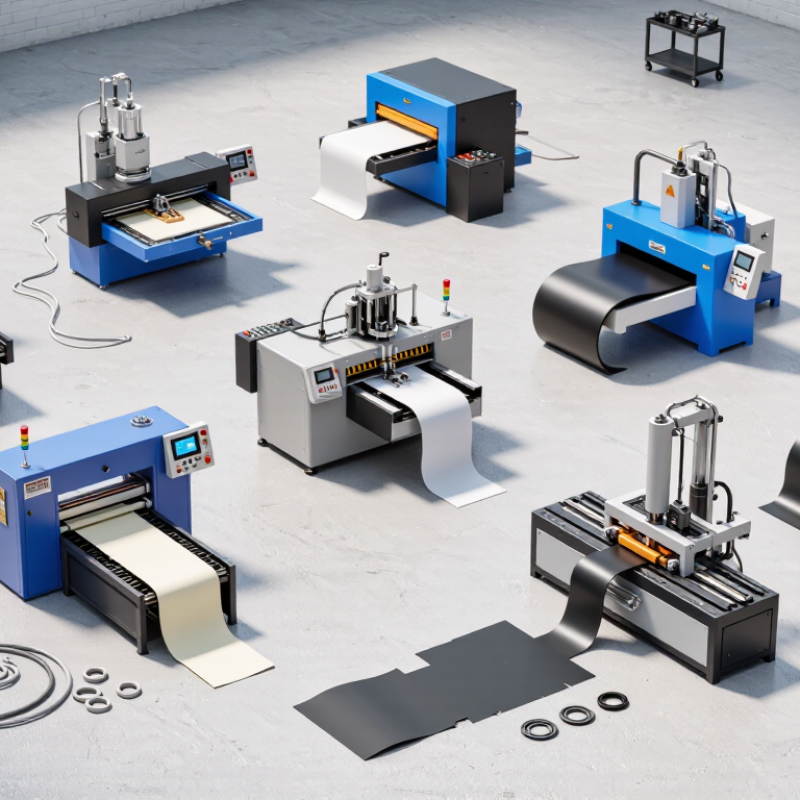
This comparison covers common automated cutting-machine types used for rubber products. “Best fit” depends on the material form, part geometry, production volume, tolerances, and required edge quality; it is not a brand ranking.
| No. | Machine type | Cutting method | Typical rubber applications | Automation and production fit | Shore A / ASTM D2240 considerations | Buyer checks |
|---|---|---|---|---|---|---|
| 1 | CNC oscillating-knife flatbed cutter | A powered blade moves rapidly up and down while following programmed contours. | Gaskets, seals, foam rubber, sheet rubber, and cut kits. | Well suited to programmed profiles, short runs, and frequent design changes; conveyor loading can support longer runs. | Hardness can affect blade choice, feed rate, and edge quality. Use Shore A as one material property, not as the sole machine-selection criterion. | Check usable cutting area, material hold-down, blade options, nesting software, and support for the required sheet thickness. |
| 2 | CNC drag-knife flatbed cutter | A knife is drawn through the material along a programmed path. | Thin rubber sheet, gasket stock, films, and flexible laminates. | Suitable for flexible materials and digitally defined parts, particularly low-to-medium volume work. | Test the actual compound: a harder or more elastic sheet may resist the blade or pull at corners differently from a softer sheet. | Review blade geometry, corner accuracy, material clamping, cutting depth control, and sample-cut results. |
| 3 | Conveyor-fed reciprocating-knife cutter | A reciprocating blade cuts programmed shapes as sheet or roll stock advances through the system. | Roll-fed rubber sheet, flexible mats, liners, and repeated component patterns. | Useful where continuous material feeding and repeatable layouts reduce manual handling. | Hardness readings can help document incoming-material variation, but the cutting program should be validated on the actual compound and thickness. | Check conveyor accuracy, roll handling, registration, waste removal, and whether the material can be held flat during cutting. |
| 4 | Automatic traveling-head clicker press | A traveling press head applies force to a cutting die positioned over the rubber. | Gaskets, washers, footwear components, and repeated shapes from sheet or board stock. | Effective for repeated die-cut shapes; automatic head positioning can reduce repositioning between cuts. | Hardness and thickness influence the force needed for a clean cut. Confirm performance using the intended die and production material. | Check available cutting force, working area, die compatibility, safety guarding, and material positioning accuracy. |
| 5 | Automatic beam or bridge press | A broad press beam descends onto a die and material to cut one or more shapes. | Large gasket patterns, rubber mats, sheet components, and footwear parts. | Can suit medium-to-high repeat production when paired with suitable feeding, positioning, and die handling. | Shore A alone does not determine press capacity; material thickness, die perimeter, compound behavior, and cut quality also matter. | Verify platen or beam coverage, pressure distribution, guarding, die changeover, and the intended cut pattern. |
| 6 | Hydraulic platen die-cut press | A platen applies controlled pressing force through a cutting die. | Rubber pads, seals, gaskets, washers, and components cut from sheet stock. | Appropriate for repeatable die cutting where the part shapes and tooling are stable. | Test cut quality across the specified Shore A range and thickness range; hardness values do not directly translate into a universal press-force setting. | Check platen size, force control, cycle and loading arrangements, die clearance, and operator safety systems. |
| 7 | Rotary die cutter | A cylindrical die cuts moving material as it passes through a rotary cutting station. | Continuous rubber strips, repeated profiles, labels, thin gasket stock, and roll-fed parts. | Best suited to stable, repeatable patterns and continuous or high-volume processing. | Material thickness, compressibility, and hardness affect die engagement and cut-through. Validate the setup with the actual roll stock. | Review roll width, die availability, registration control, changeover needs, and waste handling. |
| 8 | Automatic roll slitter and rewinder | Rotary or razor-style blades divide rubber rolls into narrower strips while the material is unwound and rewound. | Rubber strip, tape, sheet rolls, and continuous narrow profiles. | Designed for longitudinal slitting and roll processing rather than intricate individual part shapes. | Hardness and elasticity can affect edge distortion and winding tension. Evaluate edge quality at the intended material width and roll tension. | Check slitting method, roll diameter and width capacity, tension control, edge alignment, and blade-change requirements. |
| 9 | Automatic guillotine or swing-beam cutter | A straight blade moves through the material to make linear cuts. | Rubber sheets, strips, blocks, and stock cut to length or width. | Useful for straight-line cuts and basic sizing; automated stops or feeding systems can improve repeatability. | Harder or thicker stock may require different blade and machine settings. Confirm that the cut remains square without excessive compression. | Check maximum material size, blade clearance, cut-length control, hold-down method, and guarding. |
| 10 | CNC waterjet cutter | A high-pressure water stream, sometimes with abrasive depending on the application, follows a programmed path. | Thick rubber sheet, large profiles, and complex shapes where mechanical tooling may be less convenient. | Suitable for programmed contours and varied part geometries; it does not require a dedicated shaped die for each profile. | Shore A does not predict waterjet performance by itself. Check cut quality, water exposure, edge condition, and material-specific process settings. | Review work envelope, water management, tolerances on the intended material, cut-edge requirements, and operating costs. |